An unsealed or poorly sealed weld seam turns an otherwise flawless vehicle repair into an aggressive rust incubator within 12 to 18 months. When body panels, hem flanges, or floor pans flex during road operation, microscopic voids in a rigid or brittle sealant allow ambient moisture, road salt, and acidic exhaust condensates to penetrate deep into spot-welded lap joints. Consequently, the result is catastrophic: paint blistering on exterior body lines, interior cabin dampness, cabin NVH degradation, and premature structural failure. Ultimately, these defects destroy customer trust and trigger expensive warranty comebacks.
How to Achieve Factory-Grade OEM Seam Sealer Finishes
Automotive body engineers know that applying automotive seam sealer is never merely cosmetic caulking. Instead, it is a critical electrochemical barrier, acoustic dampener, and joint reinforcement element. Drawing upon decades of chemical manufacturing experience supplying commercial vehicle assemblers, OEM body shops, and global collision networks across Europe, North America, the Middle East, and Central and South America, SHCHEMPU has engineered this comprehensive technical guide. Below, we break down the polymer chemistries, bead geometries, pneumatic spray textures, substrate preparation standards, and paintability windows. As a result, you can reproduce factory-grade OEM seam sealer finishes on every joint.
Key Takeaways
- Polymer Chemistry Dictates Failure Thresholds: 1K polyurethane (PU) offers unmatched tensile elongation and mechanical toughness; modified silane polyethers (MS Polymer / SMP) deliver zero-shrinkage, isocyanate-free safety, and immediate wet-on-wet paintability; while 2K epoxy sealers provide high-modulus structural rigidity and maximum electrochemical corrosion resistance on weld flanges.
- Replicating OEM Textures Requires Three Tooling Profiles: Factory finishes cannot be achieved with generic caulking tips. Modern vehicles require precise ribbon extrusion for hem flanges, controlled nylon-bristle brushing for trunk floors and strut towers, and multi-chamber pneumatic atomization for textured underbody spray seals.
- Substrate Hierarchy and Paintability Windows: Never apply seam sealer over bare untreated steel without a certified epoxy or e-coat primer. Curing mechanisms govern paint compatibility: solvent-borne primers require adequate flash times before sealer application, while sealer skinning behavior determines whether bake cycles will cause paint cracking or solvent entrapment.
Why Automotive Seam Sealers Are Critical to Vehicle Integrity and NVH
Automotive seam sealer forms an elastomeric protective bridge across overlapping body panels that withstands continuous structural torsional vibration, preventing capillary moisture intrusion into weld seams that would otherwise initiate crevice corrosion within 500 hours of cyclic salt spray exposure.
Environmental Barrier Against Moisture, Road Salt, and Exhaust Fumes
During stamped sheet metal fabrication and robotic resistance spot welding, modern vehicle unibodies feature thousands of linear inches of overlapping steel and aluminum flanges. However, these lap joints are inherently vulnerable. Without an elastomeric barrier, atmospheric condensation, splash water, de-icing chemicals (such as magnesium chloride), and exhaust particulates are drawn into the capillary gaps between sheet layers. Therefore, high-grade automotive body seam sealers fill these dimensional tolerances completely. As a result, they isolate sensitive weld nuggets from electrochemical oxidation and create a hermetic seal that maintains passenger compartment climate control integrity.
Galvanic and Crevice Corrosion Prevention in Lap Joints and Hem Flanges
In multi-material vehicle architectures where ultra-high-strength steel (UHSS), galvanized mild steel, and aluminum alloys meet, the risk of galvanic corrosion escalates exponentially. For example, when bare spot welds are left exposed to electrolyte solutions, rapid galvanic pitting occurs. A dedicated automotive seam sealer therefore acts as an electrically insulating dielectric barrier. Moreover, when properly applied over e-coated or epoxy-primed hem flanges on doors, hoods, and decklids, the sealer encapsulates the raw metal edge. Consequently, it eliminates edge corrosion and prevents paint lift along exterior cosmetic perimeter lines.
Acoustic Damping and NVH (Noise, Vibration, Harshness) Attenuation
Automotive bodies act as acoustic resonators. Without dissipation, road excitation, tire hum, and drivetrain harmonics transmit directly through structural sheet metal. However, by engineering seam sealers with optimized loss factors ($tan\,\delta$) across typical operating temperature bands (-40°C to +90°C), manufacturers utilize the cured bead to absorb shear deformation between vibrating panels. As a result, this provides substantial dampening across floor pans, firewalls, and wheel tubs, significantly reducing interior decibel ratings compared to unsealed assemblies. Furthermore, for heavy-duty applications requiring expanded movement accommodation, builders often pair these solutions with high-elasticity polyurethane joint sealants or exterior RV body and roof sealants.
| Vehicle Zone | Primary Stress Profile | Environmental Exposure | Critical Seam Sealer Function |
|---|---|---|---|
| Door Hem Flanges | Slam fatigue & edge flex | High humidity, salt wash | Edge encapsulation, corrosion barrier, Class-A paint finish |
| Wheel Arches & Underbody | Gravel impingement & chassis twist | Direct gravel strike, water spray | Abrasion resistance, stone-chip absorption, textured spray seal |
| Floor Pans & Trunk Wells | Panel drumming, low flex | Occasional condensation, oil mist | Acoustic damping, wide-overlap water barrier, brushed finish |
| Strut Towers & Firewalls | Severe multi-axis vibration | Engine bay thermal cycling (-30°C to 110°C) | High lap shear strength, thermal stability, noxious gas barrier |
| Roof Ditches & C-Pillars | Diagonal body torsion | Direct UV radiation, thermal expansion | Zero shrinkage, UV resistance, smooth leveling under clear coat |
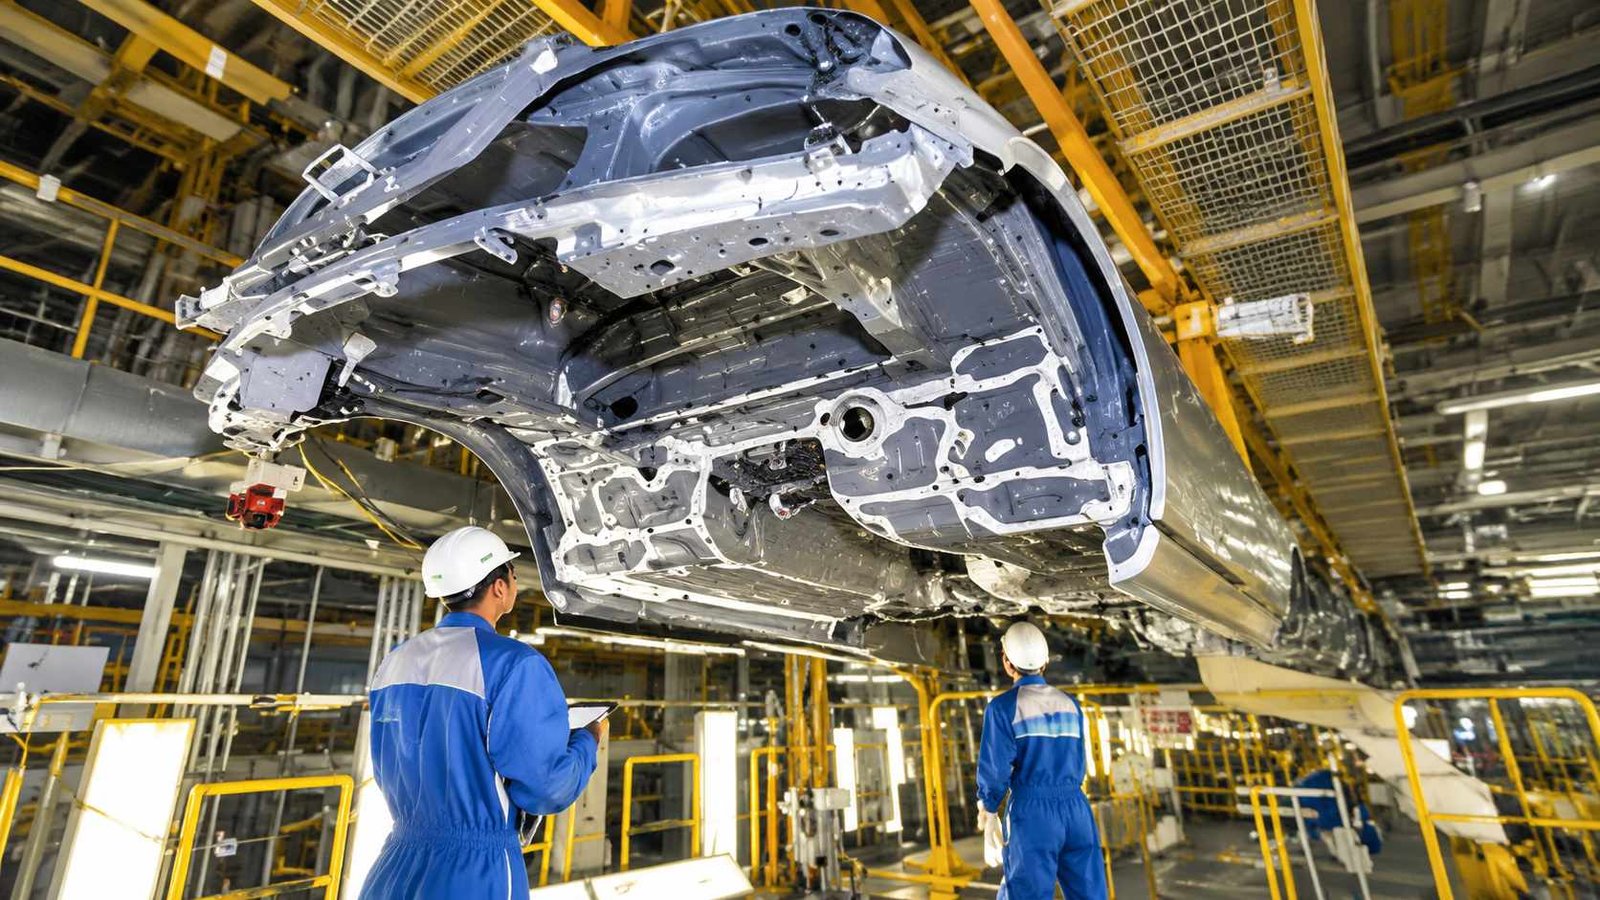
Polymer Chemistries Explained: 1K PU, MS Polymer, 2K Epoxy, and PVC Plastisol
Selecting the correct base polymer is the single most critical decision in body construction: MS Polymers have emerged as the industry benchmark for collision repair due to their zero-shrinkage chemistry and instant paintability, while 1K Polyurethanes dominate high-abrasion truck body seams, and 2K Epoxies provide structural joint reinforcement.
1K Polyurethane (PU): Tensile Toughness and Elastic Resilience
One-component moisture-curing polyurethane sealants have served as the traditional workhorse of the automotive industry for over four decades. Formulated from prepolymers with reactive isocyanate end-groups, 1K PUs react with ambient relative humidity to form a cross-linked rubber network. As a result, their hallmark attributes include remarkable tear resistance, high tensile elongation (frequently exceeding 400% to 600%), and superb abrasion resistance against stone chipping. However, standard PUs require a skinning and partial cure period before paint application. Spraying solvent-based topcoats over uncured PU can trap released carbon dioxide gas, causing unsightly micro-blistering. For projects requiring technical data, explore our comparative guide on PU vs Epoxy vs MS Polymer seam sealers.
MS Polymer (Modified Silane / SMP): The Modern OEM & Bodyshop Benchmark
Modified Silane Polymers (also referred to as Silyl-Modified Polymers or SMP) represent the cutting edge of automotive adhesive technology. Featuring a flexible polyether backbone terminated with moisture-reactive alkoxysilane groups, MS polymers cure without producing carbon dioxide. Consequently, this unique chemical architecture delivers three decisive advantages:
- Immediate Wet-on-Wet Paintability: Water-borne and solvent-borne automotive basecoats can be sprayed virtually immediately after sealer application without wrinkling or curing inhibition.
- Isocyanate and Solvent-Free: Zero VOC shrinkage guarantees that bead dimensions and spray textures remain perfectly stable after cure, preventing “telegraphing” on exterior sheet metal.
- Superior UV and Thermal Stability: Unlike conventional urethanes that can yellow or chalk under intense sun exposure, MS polymers maintain elastic integrity even when left unpainted in exterior commercial vehicle roof gutters or chassis joints.
2K Epoxy and Acrylic Hybrids: High Modulus Structural Sealing
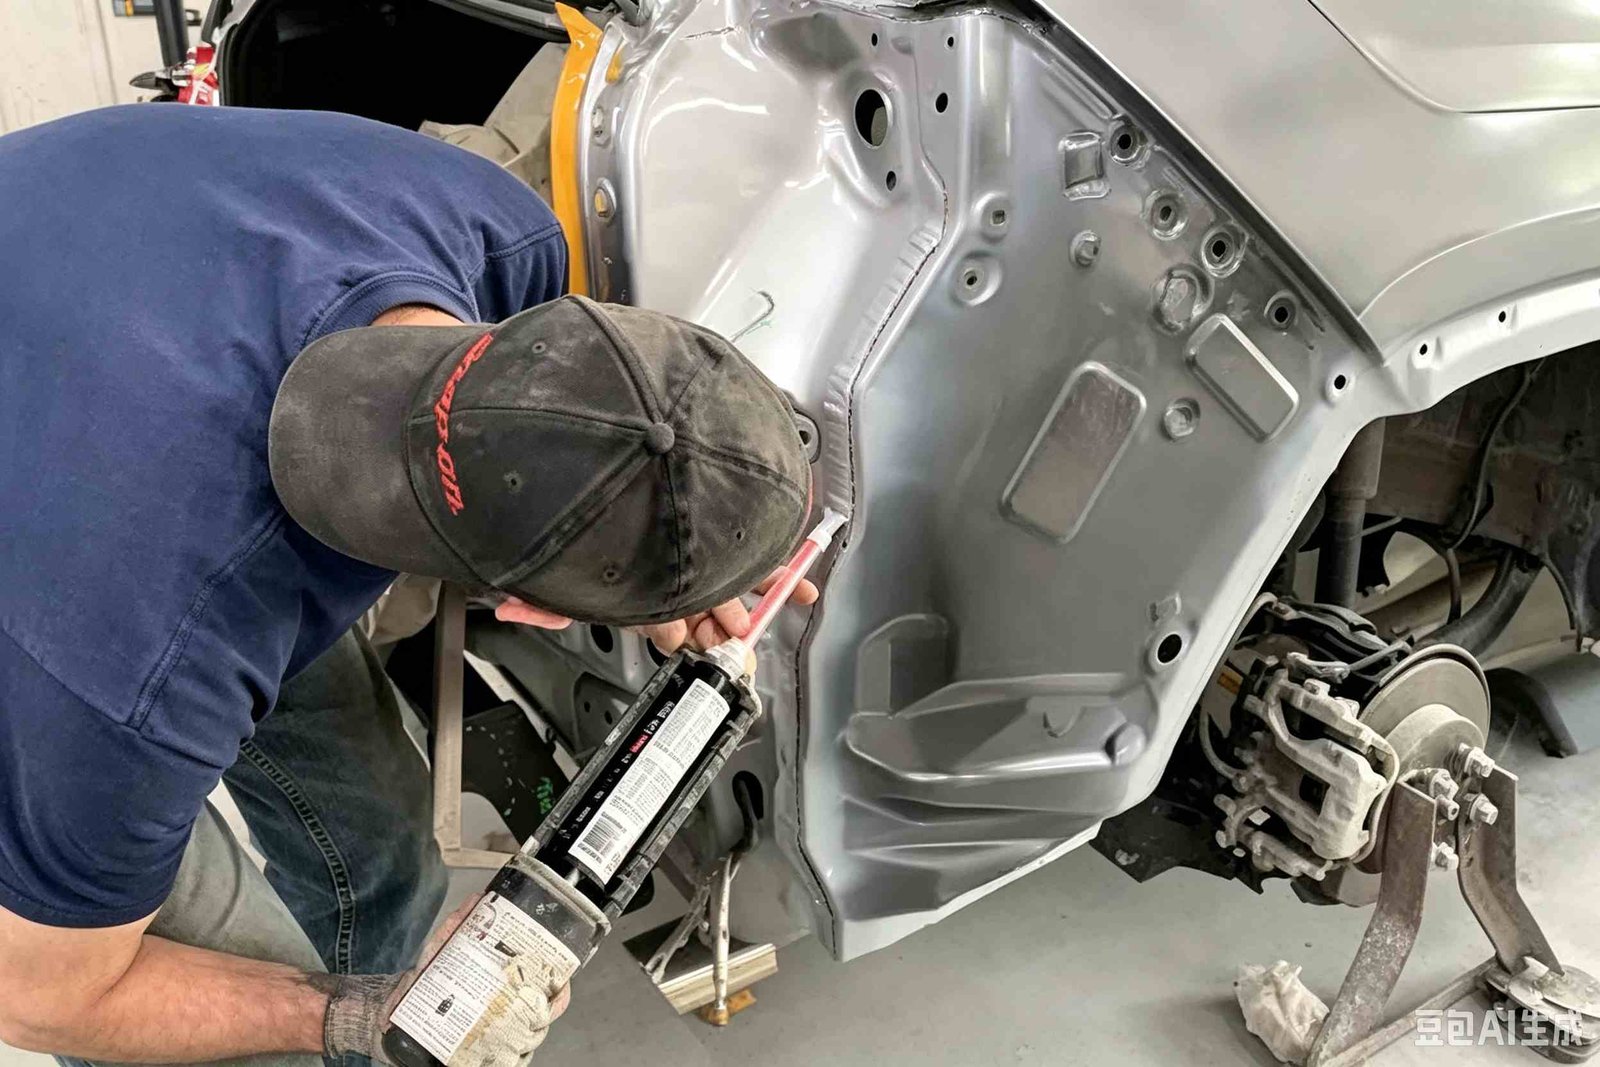
Two-component epoxies and toughened acrylics are utilized when a joint demands both environmental sealing and significant load-bearing capacity. Dispatched through static mixing nozzles, 2K systems cure independently of atmospheric humidity, achieving full functional strength within 30 to 60 minutes. Moreover, they exhibit tensile lap shear strengths exceeding 10 to 15 MPa, making them the standard choice for weld bonding, hem flange adhesive bonding, and rear quarter panel structural seams. However, while less flexible than 1K PU or MS polymers, their extreme adhesion to bare metal and e-coat prevents micro-movement along structural crush zones.
PVC Plastisols: High-Volume OEM Heat-Cured Systems
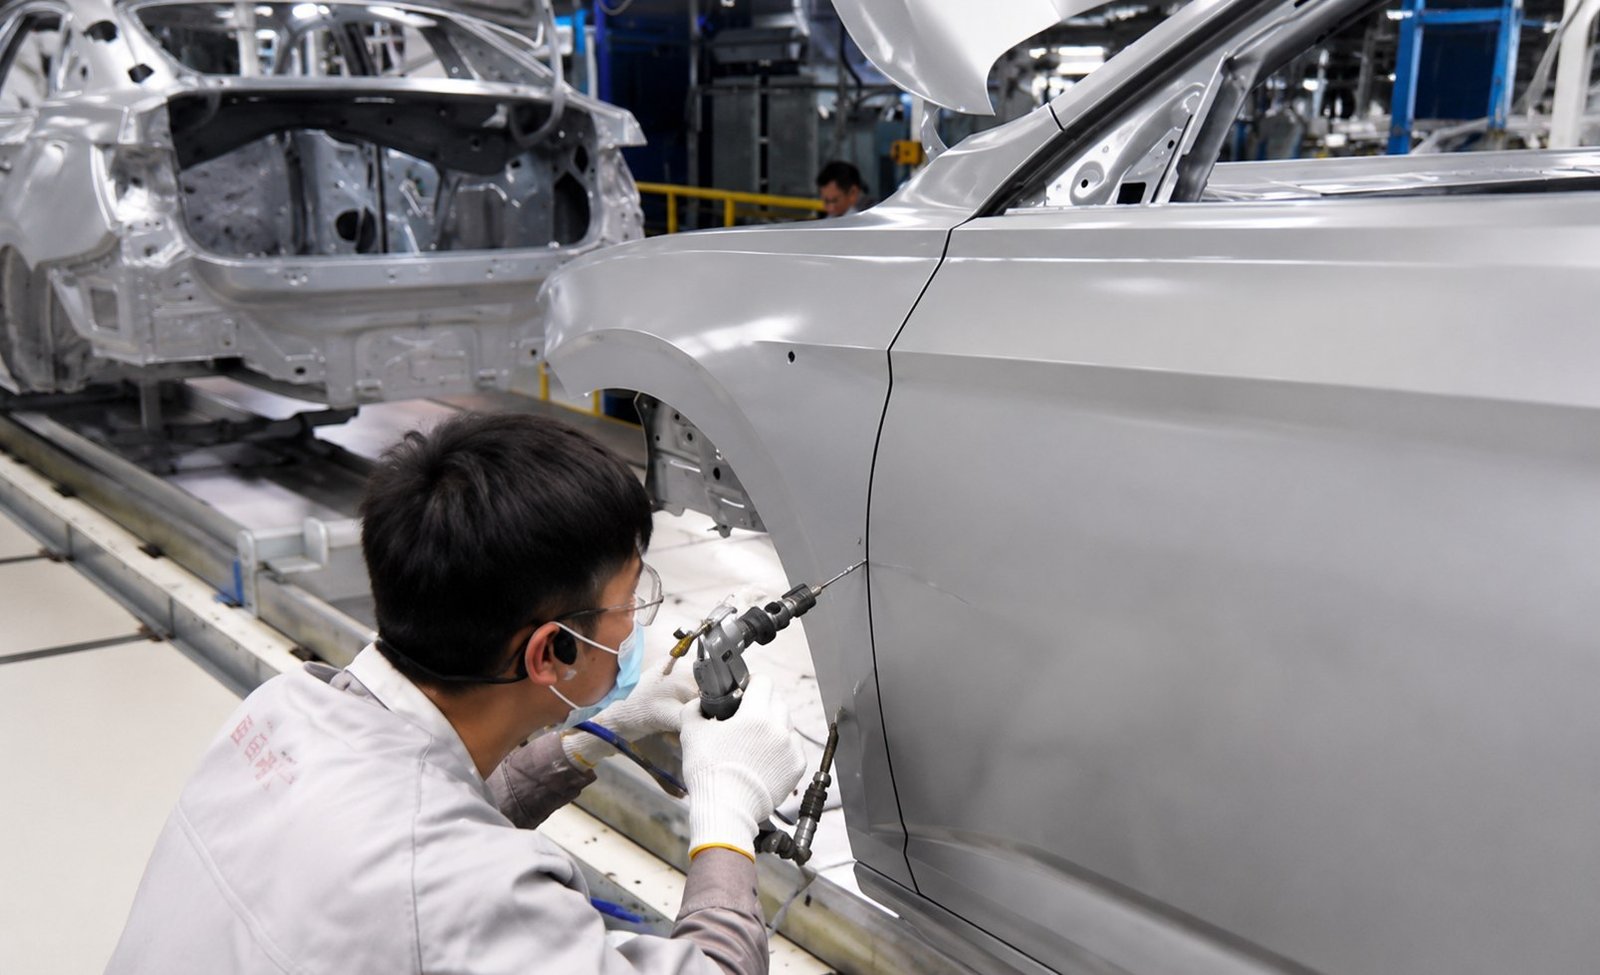
Within high-speed automotive assembly plants, automated robots dispense PVC plastisol seam sealers directly onto oily sheet metal in the body-in-white (BIW) shop. These paste suspensions of PVC resin in plasticizers do not cure at ambient room temperature. Instead, they undergo gelation and fusion when traversing the e-coat and paint baking ovens at temperatures between 140°C and 180°C. However, while cost-effective for million-unit OEM production lines, PVC plastisols cannot be used in aftermarket repair shops or secondary assembly lines where high-temperature cure ovens are unavailable.
| Performance Property | 1K Polyurethane (PU) | MS Polymer (SMP) | 2K Epoxy Sealer | PVC Plastisol (OEM) |
|---|---|---|---|---|
| Cure Mechanism | Moisture cure | Moisture cure (silane) | Chemical 2K reaction | Oven heat fusion (160°C) |
| Tensile Strength (MPa) | 2.5 – 4.0 MPa | 2.0 – 3.5 MPa | 10.0 – 20.0 MPa | 3.0 – 6.0 MPa |
| Elongation at Break (%) | 400% – 600% | 300% – 500% | 10% – 50% | 150% – 300% |
| Paintability Window | After skin forms (1–2 hrs) | Immediate wet-on-wet | 30–60 min after mix | Post-oven cooling |
| Volume Shrinkage | 2% – 5% | < 1% (virtually zero) | < 0.5% | Variable upon bake |
| UV Resistance (Unpainted) | Moderate (needs paint) | Excellent (non-yellowing) | Poor (chalks under UV) | Moderate |
| Primary Application | Bus, truck & RV bodies | Collision repair & OEM | Hem flanges & structural | High-speed OEM BIW lines |
Need custom shore hardness, cure speeds, or TDS reports for your assembly line?
Application Methods & Tooling: Master Extruded, Brushable, and Sprayable Finishes
Vehicle manufacturers utilize distinctive bead textures across different chassis regions. Replicating an OEM finish requires synchronizing material viscosity, specialized applicator nozzles, and atomizing pneumatic pressure—from narrow ribbon beads to wide textured spray passes.
Extruded Beads: Round Beads, Flat Ribbons, and OEM Profiling
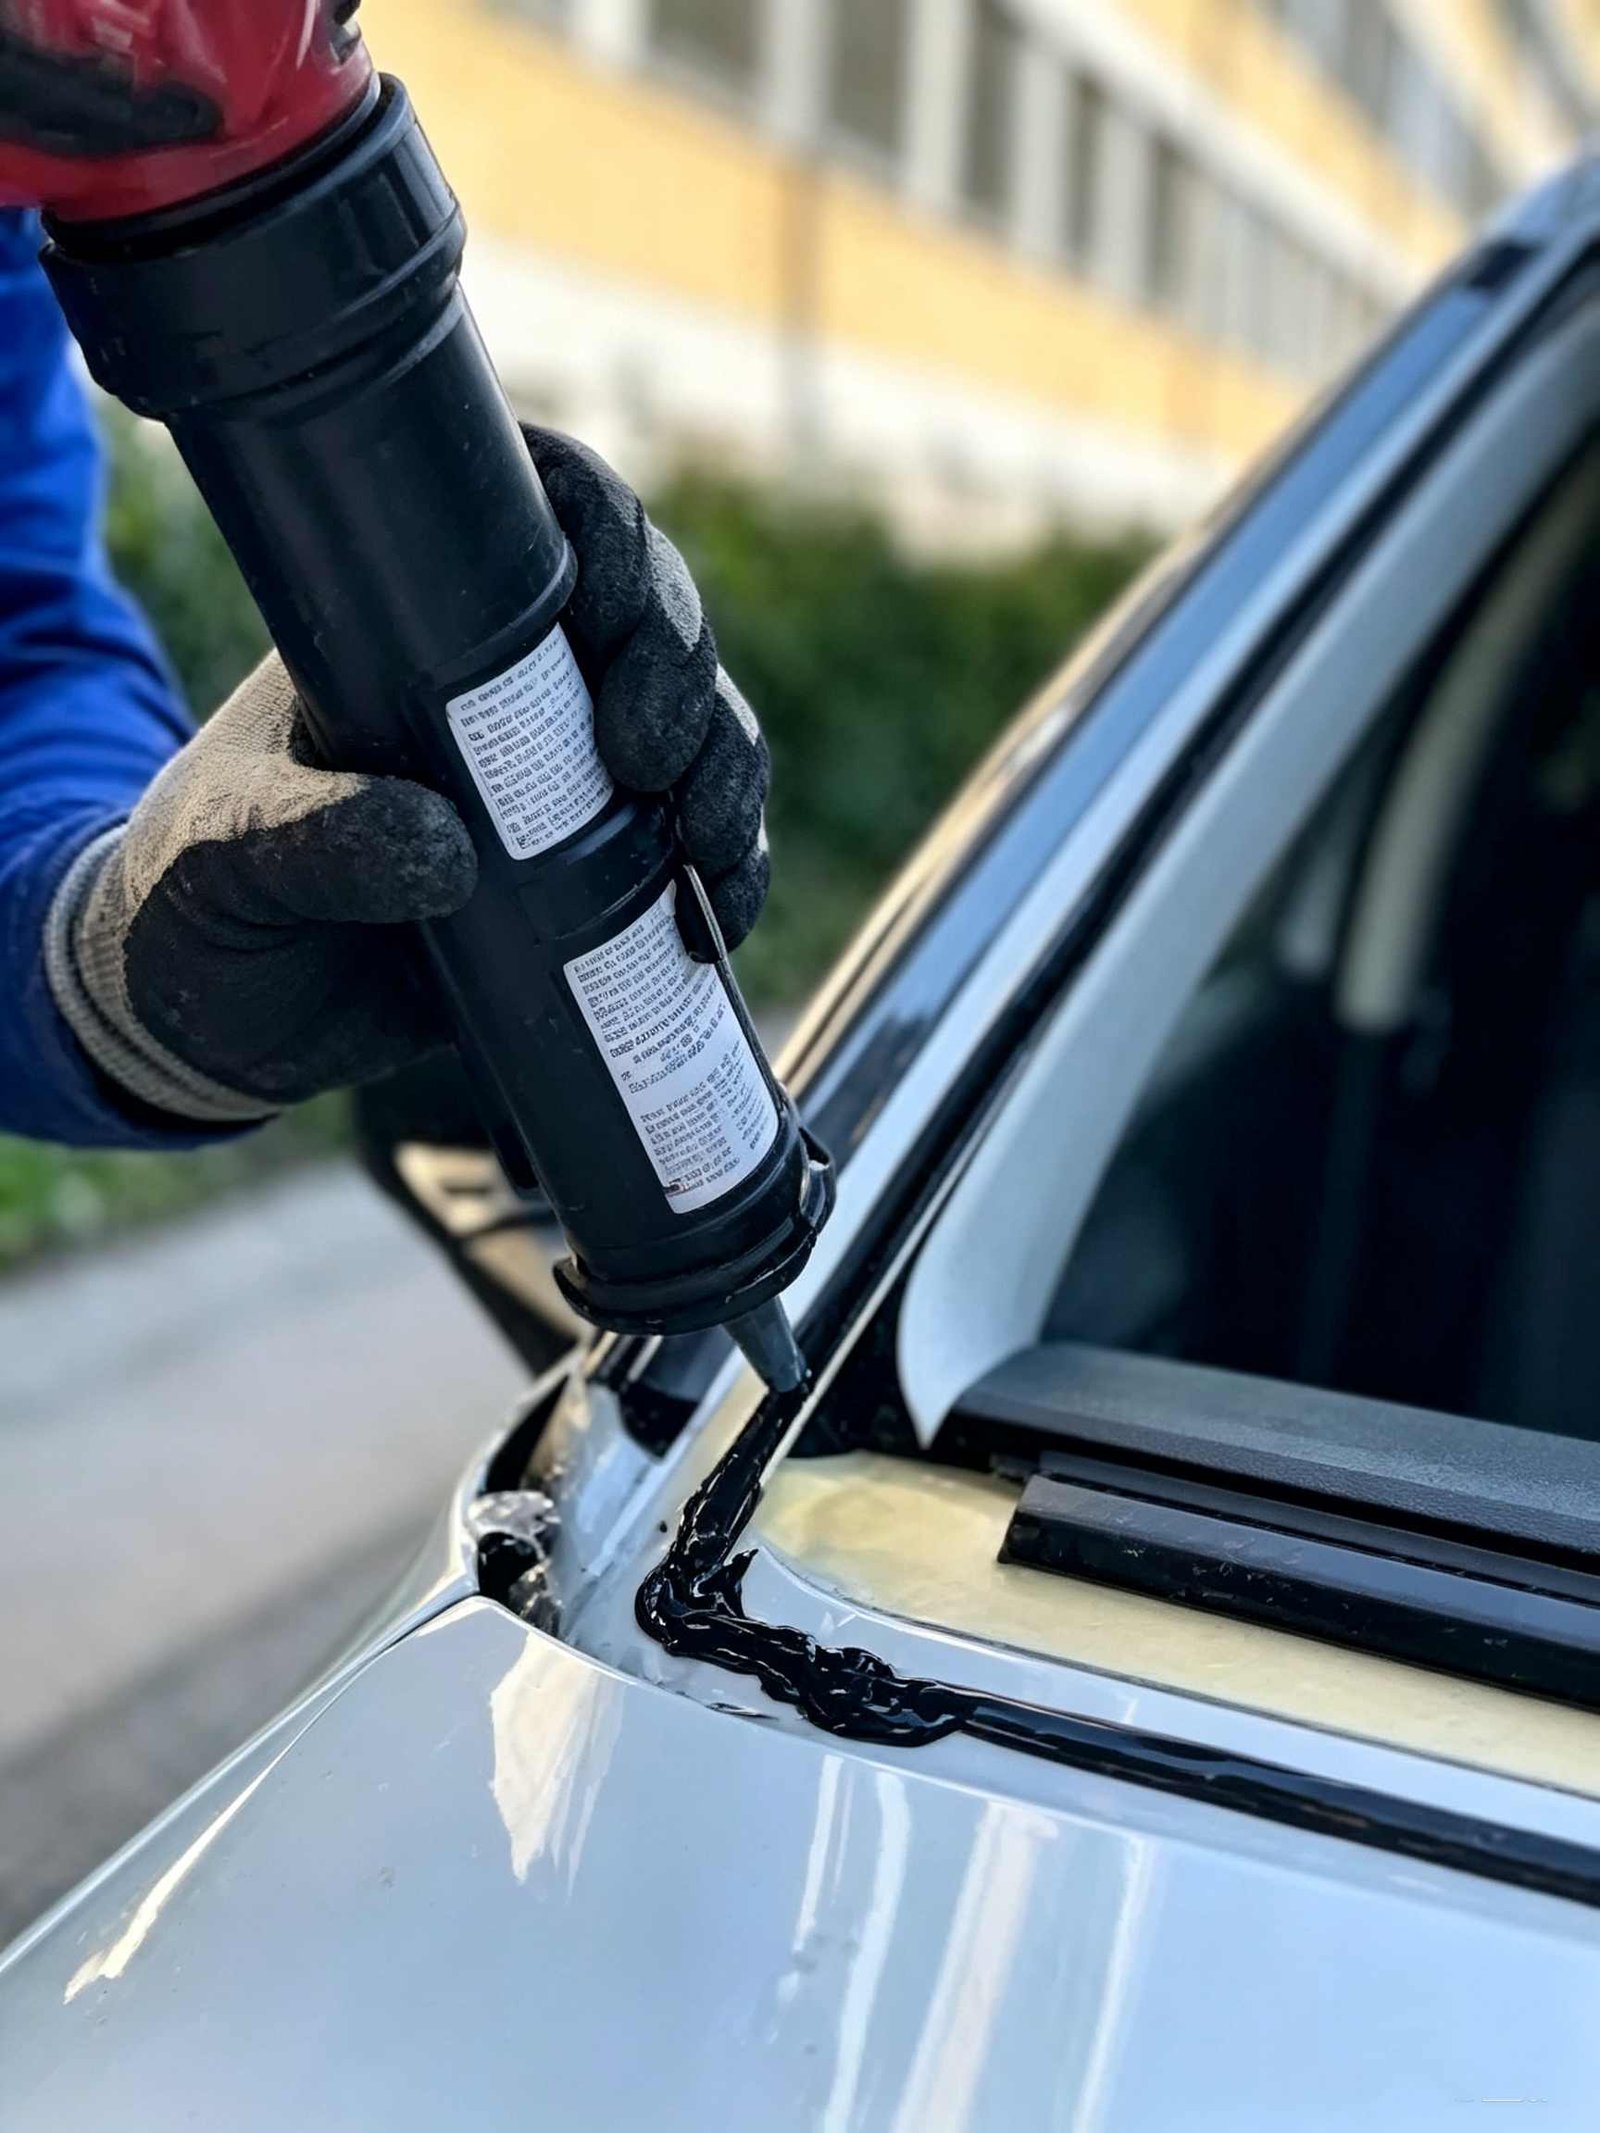
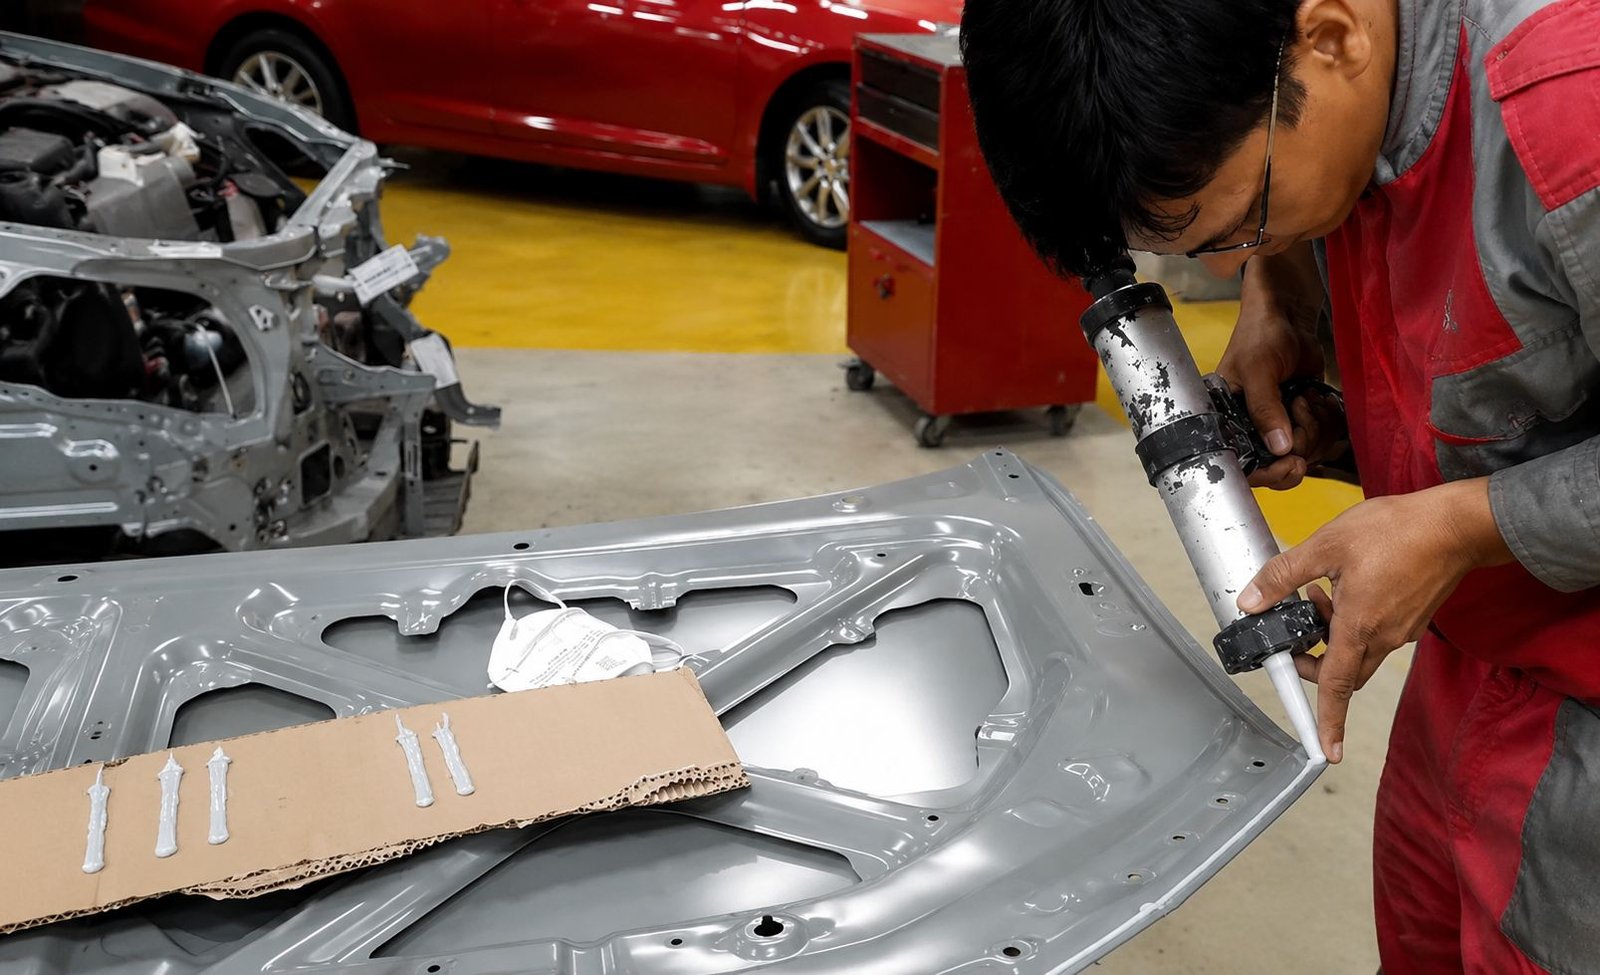
Extrusion represents the most common application technique. For straight joint overlaps, a standard round nozzle delivers a uniform cylindrical bead between 4mm and 8mm in diameter. However, on door hem flanges and decklid edges, European and Asian vehicle manufacturers predominantly specify flat ribbon beads. This finish is executed using specialized rectangular slot nozzles or pre-formed guide tips that center the nozzle over the panel lip. As a result, it extrudes a flat 10mm to 15mm ribbon with crisp beveled shoulders in a single continuous pass. In addition, proper gun angle (typically 45° to 60°) and steady traverse speed prevent bead scalloping or internal air voids. Discover our full line of professional manual, pneumatic, and cordless applicators in our sealant accessory tools catalog and our comprehensive caulking gun buying guide.
Brushable Seam Sealers: Duplicating Trunk Floor and Strut Tower Brush Marks
In luggage compartments, rear body panels, and suspension shock towers, original equipment manufacturers frequently utilize brush-finished sealers. These heavy-bodied, thixotropic sealers are designed to be leveled using a stiff nylon or hog-bristle brush. First, the technique involves extruding a generous foundation bead. Next, technicians immediately work the material across the joint with firm, unidirectional strokes. Meanwhile, the viscosity is engineered to retain distinct brush track ridges without sagging on vertical seams, replicating the hand-worked appearance common in German and Japanese manufacturing.
Sprayable Seam Sealers: Controlled Texture Atomization for Wheel Arches and Underbody
Recreating factory underbody stone-chip protection and textured rocker panel seams requires a dedicated pneumatic spray seam sealer gun. Unlike conventional paint guns that rely on high-volume low-pressure (HVLP) liquid atomization, pneumatic seam sealer guns utilize independent dual-regulator controls. One circuit pressurizes the material piston to drive viscous sealant forward. Meanwhile, a secondary air cap circuit injects atomizing air at the nozzle tip. By balancing product extrusion rate against atomizing pressure (typically 2.0 to 4.5 bar), technicians can effortlessly alternate between a narrow textured bead, a coarse orange-peel spatter, or a broad ripple coat. For step-by-step pneumatic calibration, consult our deep dive on OEM seam sealer application methods and spray textures.
| Application Style | Tooling Required | Air Pressure (Bar) | Typical Bead Thickness | Visual Appearance |
|---|---|---|---|---|
| Standard Round Bead | Manual / Pneumatic gun + Conical tip | 2.0 – 3.0 bar | 3.0 – 6.0 mm | Smooth, semi-circular uniform bead |
| Flat Ribbon Bead | Pneumatic gun + Slotted guided nozzle | 3.0 – 4.0 bar | 1.5 – 2.5 mm (12–18mm wide) | Crisp, rectangular factory tape appearance |
| Brushed Seam | Dispensing gun + Stiff nylon/nylon-wire brush | Manual tooling | 1.0 – 2.0 mm feathered edge | Pronounced linear bristle striations |
| Textured Spray Bead | Dual-regulator pneumatic spray gun | Material: 3.5 bar / Air: 2.5 bar | 1.5 – 3.0 mm (25–40mm wide) | Fine to medium orange-peel stippled texture |
| Broad Acoustic Wave Spray | Spray gun + Wide fan atomizing cap | Material: 4.0 bar / Air: 4.0 bar | 2.0 – 4.0 mm broad coating | Coarse stone-chip / acoustic damping wave |
Vehicle Body Seam Map: Where and What to Apply
Every vehicle unibody features specific joint categories requiring tailored sealer formulations. Applying a rigid sealer on a high-flex hem flange causes edge shearing, while applying a soft caulk on an exterior cosmetic roof ditch leads to clearcoat cracking.
Door Hem Flanges, Hoods, and Tailgate Perimeter Edges
The perimeter hem flange where the outer door skin wraps around the inner structural door frame is the highest-volume warranty claim zone across global automakers. Hem flanges accumulate internal condensation that drains downward into bottom seam crevices. Therefore, applying an ultra-resilient hem flange seam sealer and anti-corrosion barrier requires a 10mm to 12mm flat ribbon bead that fully covers the raw stamped edge of the metal without encroaching on door drain holes. In addition, the material must maintain flexibility down to -40°C to withstand repetitive door-slamming kinetic impacts.
Floor Pans, Trunk Beds, and Spare Tire Wells
Floor pans consist of stamped sheet steel sections joined by continuous overlapping lap joints. These horizontal joints require heavy brushed or wide sprayed sealers that bridge gap tolerances up to 3mm. However, for commercial trailers, buses, and refrigerated delivery vans, builders frequently transition from standard seam sealers to self-leveling polyurethane or hybrid formulations, such as those found in our self-leveling joint sealant line. As a result, they ensure zero puddle accumulation and smooth floor finishing.
Strut Towers, Firewalls, and Chassis Rail Junctions
Suspension strut housings and the forward firewall represent structural unibody nodes subjected to severe torsional twisting, steering vibration, and extreme engine-compartment heat. In these regions, high-modulus 2K epoxy sealers or fiber-reinforced 1K polyurethanes are mandatory. Consequently, they reinforce structural stiffness while blocking engine fumes and heat transmission into the passenger cockpit.
Roof Ditches, Quarter Panels, and Glass Aperture Transitions
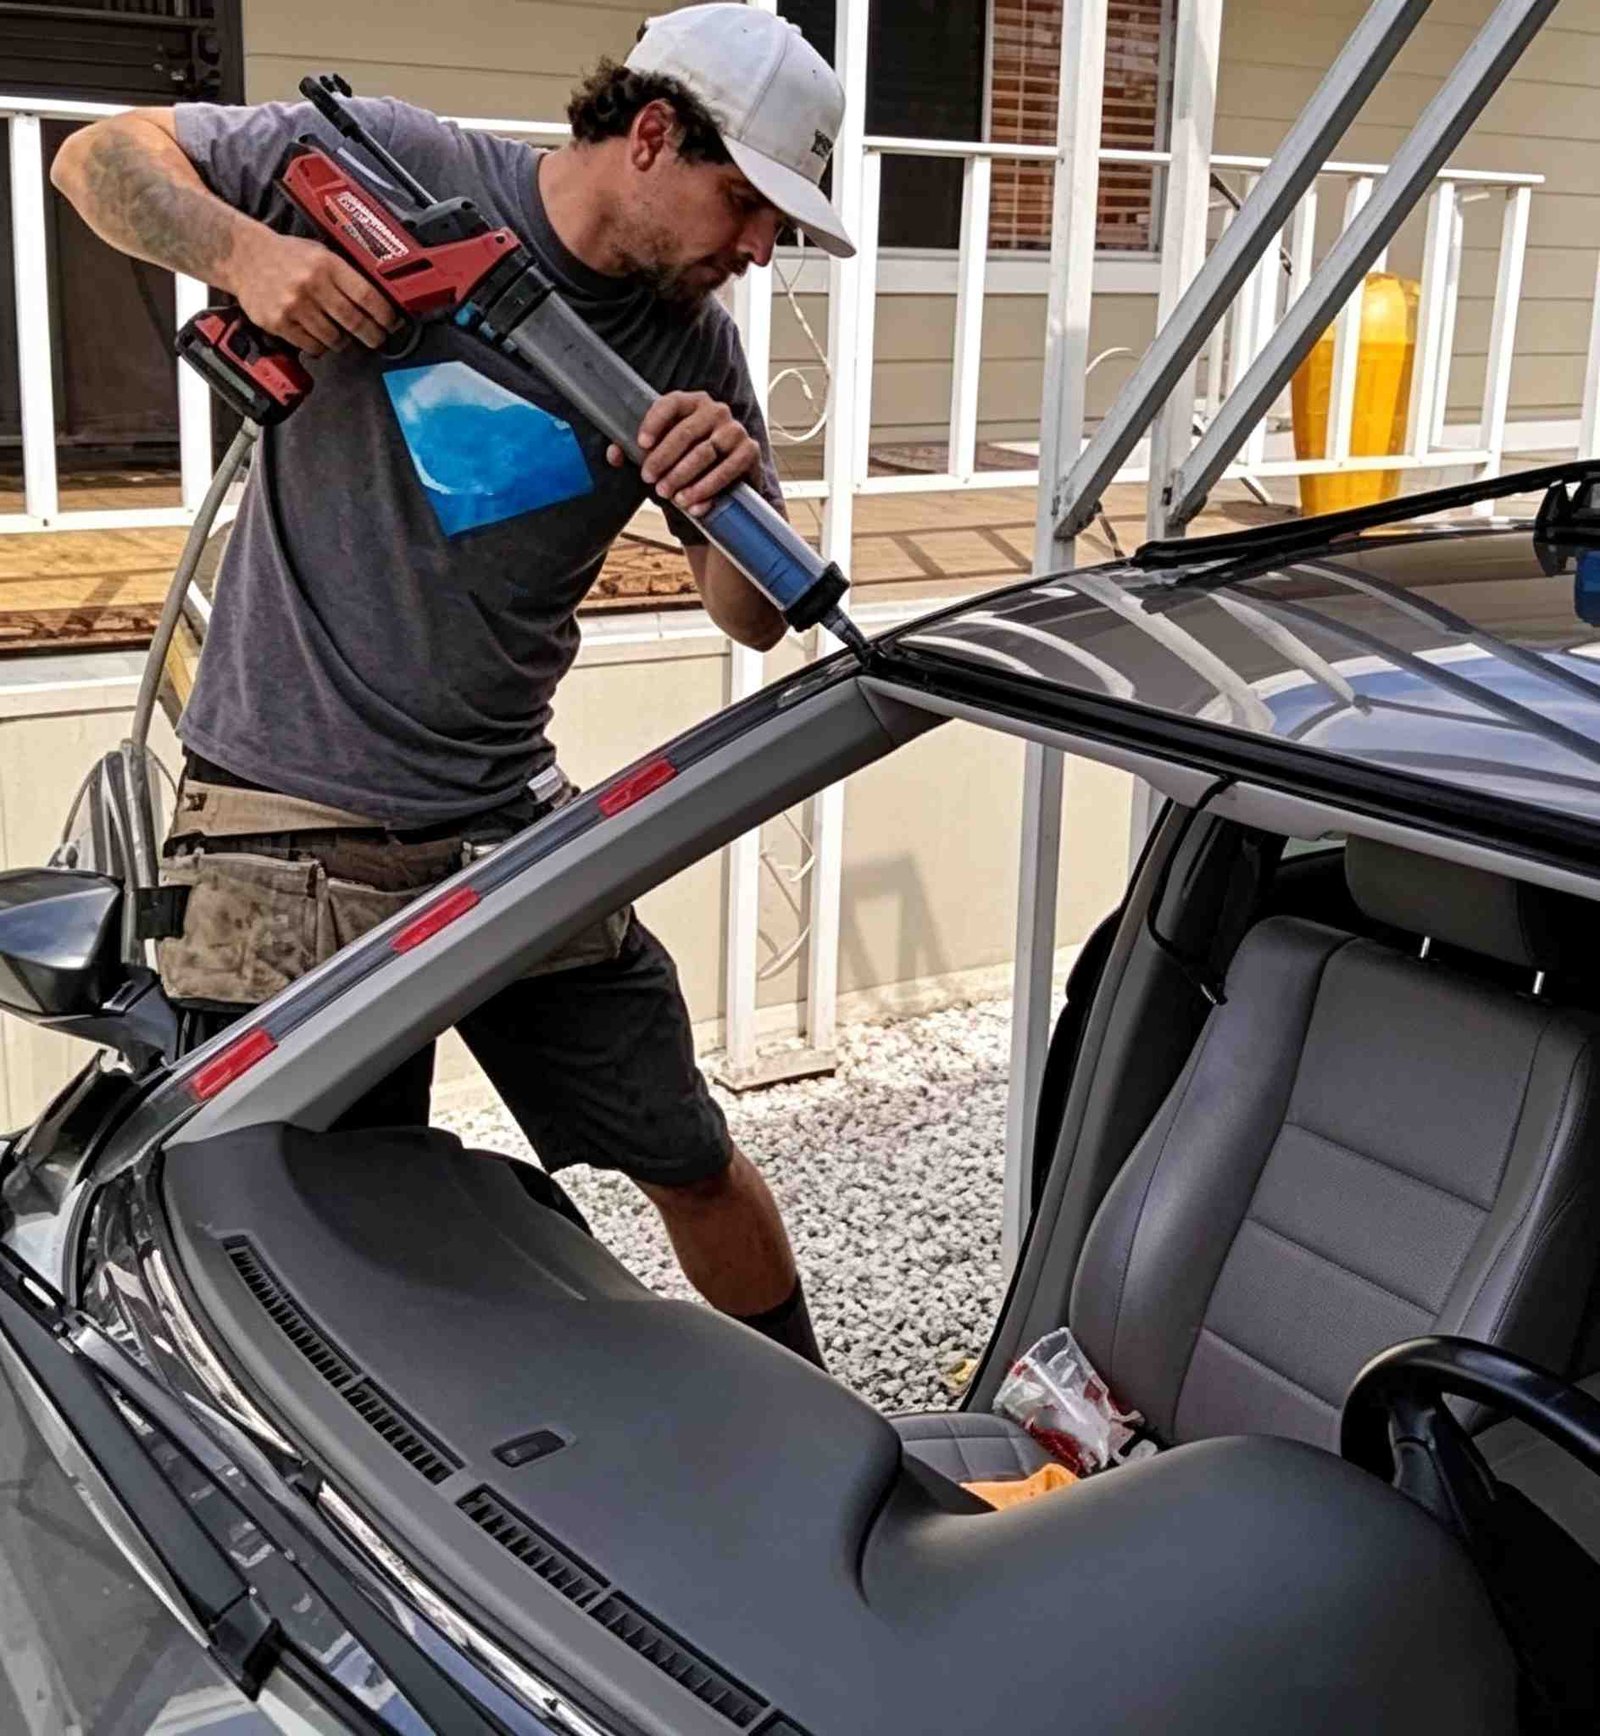
Roof ditches and rear quarter panel joints sit on Class-A visible surfaces directly beneath final paint and clearcoat layers. Therefore, they demand zero-shrinkage MS polymers that accept bake cycles without telegraphing or outgassing. Crucially, where body seams terminate at windshield and backlight pinchwelds, technicians must recognize the distinct technical boundaries between seam sealers and direct glazing adhesives. While seam sealers water-seal the pinchweld flanges, structural glass retention must always be performed exclusively using certified FMVSS-compliant polyurethane windshield adhesives with documented safe drive-away times. Review our fast-curing 30-minute windshield adhesive specifications for high-turnover glazing operations.
Surface Preparation, Primers, and the Paintability Window
Over 85% of seam sealer warranty delaminations are traced directly to surface contamination or violating the chemical paint window. Seam sealer must never be viewed as a substitute for corrosion-inhibiting primers on bare automotive steel.
The Substrate Hierarchy: Bare Steel, E-Coat, and Epoxy Primers
For optimal electrochemical protection and adhesion durability, seam sealers must be installed on properly prepared foundations:
- OEM Electrocoat (E-Coat): The gold standard substrate. Scuff with a maroon abrasive pad (equivalent to 320–400 grit) and degrease thoroughly using a non-aggressive solvent cleaner before sealer dispensing.
- 2K Epoxy Primers: The mandatory substrate over bare welded steel or aluminum repair areas. Apply 2K epoxy primer, allow complete solvent flash and initial crosslinking (minimum 4 to 8 hours depending on TDS), then apply seam sealer directly over the cured epoxy.
- Direct-to-Metal (DTM) Formulations: While certain specialized MS polymers feature DTM certification, applying sealer directly over unprimed bare steel in harsh climates is discouraged by major OEM collision standards, as it lacks the sacrificial zinc or epoxy corrosion inhibitors necessary for multi-year warranty defense.
- 1K Etch Primers: Avoid Beneath Sealers! Acidic 1K wash primers contain phosphoric acid that chemically interferes with the amine or tin catalysts in polyurethanes and MS polymers, resulting in gummy, uncured interfaces that peel effortlessly under load.
Understanding the Paintability Window: Wet-on-Wet vs Bake Cycles
The interaction between the sealant and the paint topcoat governs finish durability. For instance, when using MS polymers, modern waterborne and solvent-borne basecoats can be applied “wet-on-wet” within 20 to 60 minutes. However, if using traditional 1K polyurethanes, technicians must allow the outer skin to form thoroughly (typically 60 to 120 minutes at 23°C and 50% relative humidity) before paint booth entry. Otherwise, introducing fresh, solvent-laden paint over uncured PU into a heated 60°C spray booth bake cycle accelerates solvent boiling and trapped gas expansion, generating catastrophic paint micro-pinholes.
| Substrate Type | Surface Prep Requirement | Primer Mandatory? | Adhesion Performance Rating |
|---|---|---|---|
| OEM Factory E-Coat | Scuff with maroon pad + Solvent degrease | No (Direct application approved) | Exceptional (100% cohesive failure) |
| 2K Epoxy Primer | Fully cured, degreased, light scuff if aged > 48 hrs | Already primed | Optimal OEM standard for collision repair |
| Bare Sanded Carbon Steel | P80–P180 disc sand + Acetone/alcohol degrease | Yes (2K Epoxy primer required) | Poor without primer (high crevice rust risk) |
| Galvanized Sheet Steel | Fine nylon abrasive scuff + Solvent wash | Recommended (Epoxy or DTM MS polymer) | Good; susceptible to white rust if unsealed |
| Aluminum 5000/6000 Series | Stainless wire brush/pad + Non-chlorinated solvent | Yes (Epoxy primer within 1 hr of deoxidation) | Excellent when aluminum oxide layer is controlled |
| 1K Acid Etch Wash Primer | Avoid direct sealer contact | Must be sealed with 2K surfacer first | Incompatible (cure inhibition & peeling) |
Troubleshooting: 7 Common Seam Sealer Failures and Preventive Actions
When a seam sealer cracks, blisters, or peels, the root cause is almost always procedural rather than a defect in chemical manufacturing. Below are the seven most common seam sealer failure modes observed in field warranty inspections and their exact remedies.
1. Paint Blistering and Micro-Pinholes Over the Cured Bead
Root Cause: Premature paint application over uncured 1K polyurethane sealer followed by heated booth baking. The heat forces rapid evaporation of retained solvents and reaction CO2 gas. Consequently, pinholes blow through the wet paint film. Corrective Action: Switch to zero-VOC MS polymers or ensure minimum 2-hour ambient cure at 23°C/50%RH for polyurethanes prior to oven cycling.
2. Longitudinal Bead Cracking and Splitting Down the Joint Centerline
Root Cause: Excessive joint movement exceeding the tensile elongation limits of the cured material, or three-point bonding where sealant adheres to the bottom of the joint gap rather than only the opposing panel sides. Corrective Action: Select high-elongation sealants (>400%) or utilize polyethylene bond-breaker tape in deep dynamic seams.
3. Complete Adhesive Delamination (Peeling like Tape)
Root Cause: Surface contamination by stamping oils, silicone tire dressing residue, sanding dust, or direct application over 1K etch primer. Corrective Action: Enforce two-cloth solvent cleaning protocols and only apply over verified e-coat, 2K epoxy, or clean scuffed metal.
4. “Telegraphing” / Shadow Shrinkage Lines on Exterior Quarter Panels
Root Cause: Solvent evaporation shrinkage in high-solvent sealants, or thermal contraction pull after baking. Corrective Action: Mandate 100% solids, solvent-free MS polymer chemistry that retains 100% of its wet volume upon complete cure.
5. Orange Peel and Spatter Mismatch in Sprayable Applications
Root Cause: Incorrect pneumatic gun balance or incorrect nozzle-to-panel distance. Too much atomizing air creates powdery overspray; too little air causes large irregular clumps. Corrective Action: Test spray onto scrap cardboard to calibrate material feed vs atomizing air ratio before touching vehicle metal.
6. Air Voids and Pinholes within the Bead Core
Root Cause: Rapid jerky gun movement, improper nozzle angle, or dragging the nozzle through the applied bead. Corrective Action: Maintain a 45-degree push angle with continuous material extrusion ahead of the nozzle tip.
7. Soft Paint Syndrome (Tacky Paint That Never Dries Over the Bead)
Root Cause: Plasticizer migration from low-grade sealants leaching into the paint film, preventing complete catalyst cure of clearcoats. Corrective Action: Formulate strictly with high-molecular-weight non-migrating plasticizers certified under automotive OEM testing.
| Observed Defect | Primary Root Cause | Immediate Shop Floor Fix | Long-Term Prevention Protocol |
|---|---|---|---|
| Micro-Bubbling in Paint | Trapped CO2 outgassing in heated bake | Sand flat, re-prime with 2K sealer | Upgrade to isocyanate-free MS polymer |
| Centerline Bead Cracking | Insufficient elongation / 3-point adhesion | Cut out bead, re-apply high-flex sealant | Use bond-breaker tape in dynamic expansion seams |
| Interfacial Peeling | Oil/wax residue or 1K acid primer contact | Strip to metal, apply 2K epoxy primer | Mandate 2-cloth solvent wipe; ban 1K etch under sealers |
| Telegraphing / Sink Lines | Solvent shrinkage during bake | Block-sand clearcoat, spot blend | Enforce 100% solids, zero-shrinkage formulations |
| Spray Texture Mismatch | Miscalibrated air/product pressure ratio | Wipe wet with solvent before tack | Use standardized pneumatic test card calibration |
SHCHEMPU Case Study: Commercial Vehicle Assembler Streamlines Body Assembly Cycle
By converting from traditional 1K polyurethanes to SHCHEMPU Advanced MS Polymer Body Sealer, a leading commercial bus and special-vehicle coachbuilder in Europe, North America, Middle East, Central and South America successfully eliminated paint micro-bubbling, transitioned to immediate wet-on-wet painting, and achieved zero weld seam corrosion returns across multi-year fleet operations.
CLIENT CHALLENGE
- Commercial transit bus and chassis coachbuilder assembling approximately 1,000+ specialized transport bodies annually.
- Using legacy 1K PU required a mandatory 3-4 hours pre-cure wait before spray booth entry, creating a severe shop-floor bottleneck.
- Consequently, heated paint bake cycles produced recurring rework of approximately 4–5%, caused by paint solvent popping along exterior roof lap seams.
OUR SOLUTION
- Engineered customized SHCHEMPU SMP-Series High-Tack MS Polymer seam sealer in 600ml sausage packaging.
- Formulated zero-VOC chemistry with customized thixotropy optimized for both extruded flat ribbons and pneumatic spray coats.
- Standardized pneumatic applicator tooling with dual-regulator pressure settings for rapid shop-floor transition.
RESULTS & VALUE
- Cycle Time Reduction: approximately 30–35% through immediate wet-on-wet topcoat application without pre-bake waiting.
- Zero Paint Blistering: As a result, paint micro-bubbling defects dropped to zero in post-bake quality inspections.
- Packaging Waste & Cost Reduction: Meanwhile, 600ml foil sausages reduced container disposal volume by approximately 70–80% and lowered per-meter applied sealant cost by approximately 20%.
Data source: SHCHEMPU Technical Field Application Audit. Note: Specific quantitative improvements vary by assembly line speed and shop climate; bracketed figures represent typical baseline operational benchmarks.
Sourcing Automotive Seam Sealers in Bulk: Packaging Economics and OEM Standards
For body shops, distributors, and manufacturing plants, selecting the optimal packaging configuration—from 310ml aluminum cartridges to 600ml foil sausages and 200L bulk drums—reduces linear meter application cost by up to 30% while curbing chemical waste.
Packaging Formats: Cartridge vs Foil Sausage vs Pail & Drum Economics
Every purchasing manager must balance labor convenience against chemical unit pricing. Standard 310ml rigid aluminum cartridges offer convenience for low-volume collision shops and mobile repair technicians. However, they leave up to 8% to 12% residual sealant in the plastic plunger base. In contrast, 400ml and 600ml aluminum foil sausages collapse completely under pneumatic drive pistons, reducing unrecovered chemical waste to less than 1.5% while delivering 30% more material per loading cycle. Meanwhile, for automated manufacturing plants and coachbuilders running robotic pump lines, 20L pails and 200L bulk drums offer the lowest price per kilogram. For complete procurement economics, explore our analysis on bulk automotive seam sealer sourcing: cartridges vs sausages vs drums.
Storage Best Practices and Shelf-Life Integrity
Because both polyurethanes and MS polymers are moisture-curing polymers, storage conditions directly dictate chemical viability. Product should be warehoused between 10°C and 25°C in unopened original packaging with relative humidity below 60%. Otherwise, exposure to high warehouse temperatures (>35°C) can initiate premature container polymer condensation, increasing extrusion viscosity and clogging pneumatic spray tips. When stored correctly, SHCHEMPU products maintain a guaranteed 12-month shelf life from the date of manufacture.
| Packaging Format | Target User Base | Material Waste % | Relative Cost / Liter | Primary Advantage |
|---|---|---|---|---|
| 310ml Cartridge | Collision shops, retail distributors | 8% – 12% | Baseline (100%) | No specialized gun required; easy partial-use storage |
| 400ml / 600ml Sausage | Fleet repairers, bus & trailer builders | < 1.5% | 75% – 82% | 80% less disposal volume, lowest cost for hand tools |
| 20L Pail / 200L Drum | Automated OEM assembly, robotic lines | < 0.5% (with follower plate) | 55% – 65% | Continuous automated dispensing, maximum cost efficiency |
SHCHEMPU Automotive Chemical Engineering Team
Technical Services & OEM Formulations · SHCHEMPU · Since 2013 (13+ years of experience) Industry Experience
SHCHEMPU specializes in high-performance polyurethane adhesives, modified silane polymers, and automated sealant filling solutions for automotive OEM assembly, collision restoration, and commercial vehicle fabrication across 40+ global export destinations. As a certified automotive adhesive manufacturer from China, we partner with engineers worldwide to deliver ISO-compliant sealing systems.
Summary: Engineering Reliable Automotive Seam Sealer Finishes
Executing durable automotive seam seals requires aligning the chemical polymer foundation with the structural flex demands of each vehicle zone, matching specialized applicator tooling to reproduce authentic OEM bead textures, and respecting surface preparation and paintability protocols.
- Select Polymer by Service Demands: Utilize MS polymers for collision repair and immediate wet-on-wet painting; deploy 1K polyurethanes for high-abrasion truck chassis joints; and specify 2K epoxies for rigid structural hem flanges.
- Standardize Tooling and Pressure Calibration: Dedicate appropriate flat ribbon nozzles for door perimeters, stiff bristle brushes for trunk pans, and dual-regulator pneumatic spray guns for underbody textures.
- Enforce Substrate Integrity: Never apply seam sealers over unprimed bare steel or 1K acid etch primers; rely on scuffed e-coat or fully cured 2K epoxy primers to guarantee multi-year electrochemical corrosion defense.
SHCHEMPU FACTORY DIRECT SUPPLY
Ready to Source High-Performance Automotive Seam Sealers?
Connect with our chemical formulation engineers to discuss custom cure profiles, private label packaging, or bulk cartridge and sausage container pricing. We provide comprehensive TDS/MSDS documentation and express sample dispatch worldwide within 24 hours.