Automotive glass technicians frequently confront severe pinchweld corrosion and wax contamination hidden beneath old polyurethane beads. Scraping through factory electrocoat paint with aggressive cutout blades exposes bare carbon steel to environmental moisture. Bonding fresh direct glazing urethane over oxidized pinchweld metal guarantees bond line detachment and catastrophic water leaks.
Executing a compliant pinchweld cleaning protocol is the most critical stage of the Auto Glass Replacement Safety Standard (AGRSS). Bonding structural glass requires a chemically pristine substrate free from road oils, silicone residues, and rust blisters.
This engineering standard operating procedure details mechanical rust remediation, chemical degreasing, and anti-corrosion barrier priming. Auto glass technicians and collision repair specialists will gain actionable instructions to passivate oxidized pinchwelds and restore factory structural crash integrity.
Executive Summary: Critical Rules for Pinchweld Surface Preparation
- The 1mm Urethane Cushion Rule: Technicians must never scrape pinchweld steel down to bare metal unless rust is present; retaining a clean, intact 1mm to 2mm base layer of OEM polyurethane provides the ideal bonding foundation.
- Mechanical Rust Abrasion: Surface rust requires complete mechanical removal using 80-grit abrasive discs or stainless steel wire wheels before chemical passivation.
- Two-Cloth Degreasing Discipline: Applying wax and grease remover windshield solvent requires wiping forward with a wet towel and immediately lifting residues with a dry microfiber cloth before solvent flashes off.
- Multi-Stage Primer Barrier: Deep cutout scratches down to bare steel mandate certified anti-corrosive pinchweld primer to halt electrochemical oxidation beneath the cured adhesive.
Corrosion Mechanisms: Why Cutout Scratches Trigger Bond Release
Pinchweld rust repair requires aggressive surface intervention. When moisture contacts unprotected carbon steel along window frames, electrochemical oxidation expands iron oxide to sixteen times its original volume.
Galvanic Corrosion and Blade Damage
Vehicle manufacturers protect body pinchwelds through multi-stage cathodic electrodeposition (E-coat) primers. During old glass cutout operations, vibrating reciprocating blades or pull knives easily slice through this protective 25-micron barrier.
Exposing bare steel to ambient moisture trapped beneath exterior moulding creates active galvanic cells. Iron atoms surrender electrons to dissolved oxygen, converting solid steel into friable iron oxide hydrate (Fe2O3·H2O).
The Delamination Wave Beneath Polyurethane Beads
Rust does not bond cohesively to structural polyurethane. As rust blisters expand beneath the adhesive bed, shear stresses peel the urethane bead upward from the steel flange. During emergency braking or passenger airbag deployment, the delaminated windshield blows outward, failing federal crash retention mandates.
Corrosion Classification: Selecting the Correct Pinchweld Remediation Level
Technicians must classify window frame damage before selecting chemical primers. The engineering matrix below defines remediation protocols across four progressive corrosion stages.
| Corrosion Severity Level | Substrate Physical Condition | Mechanical Preparation SOP | Chemical Coating Protocol |
|---|---|---|---|
| Level 1: Minor Scratches | Shallow nicks < 5 mm wide; no rust | Trim urethane to 1 mm; solvent wipe | Single coat black glass primer |
| Level 2: Surface Oxidation | Light surface rust; solid metal base | Grind with 80-grit wheel to bright steel | Zinc-rich etch primer + black primer |
| Level 3: Deep Pitting | Rough scale rust; pitted steel flange | Wire wheel scale removal; media blast | 2-part epoxy anti-corrosion primer |
| Level 4: Perforated Steel | Holes through pinchweld weld seams | Cut out compromised section completely | Weld fresh steel; full body shop paint |
Typical Application Scenarios: Workshop Realities & Rust Remediation
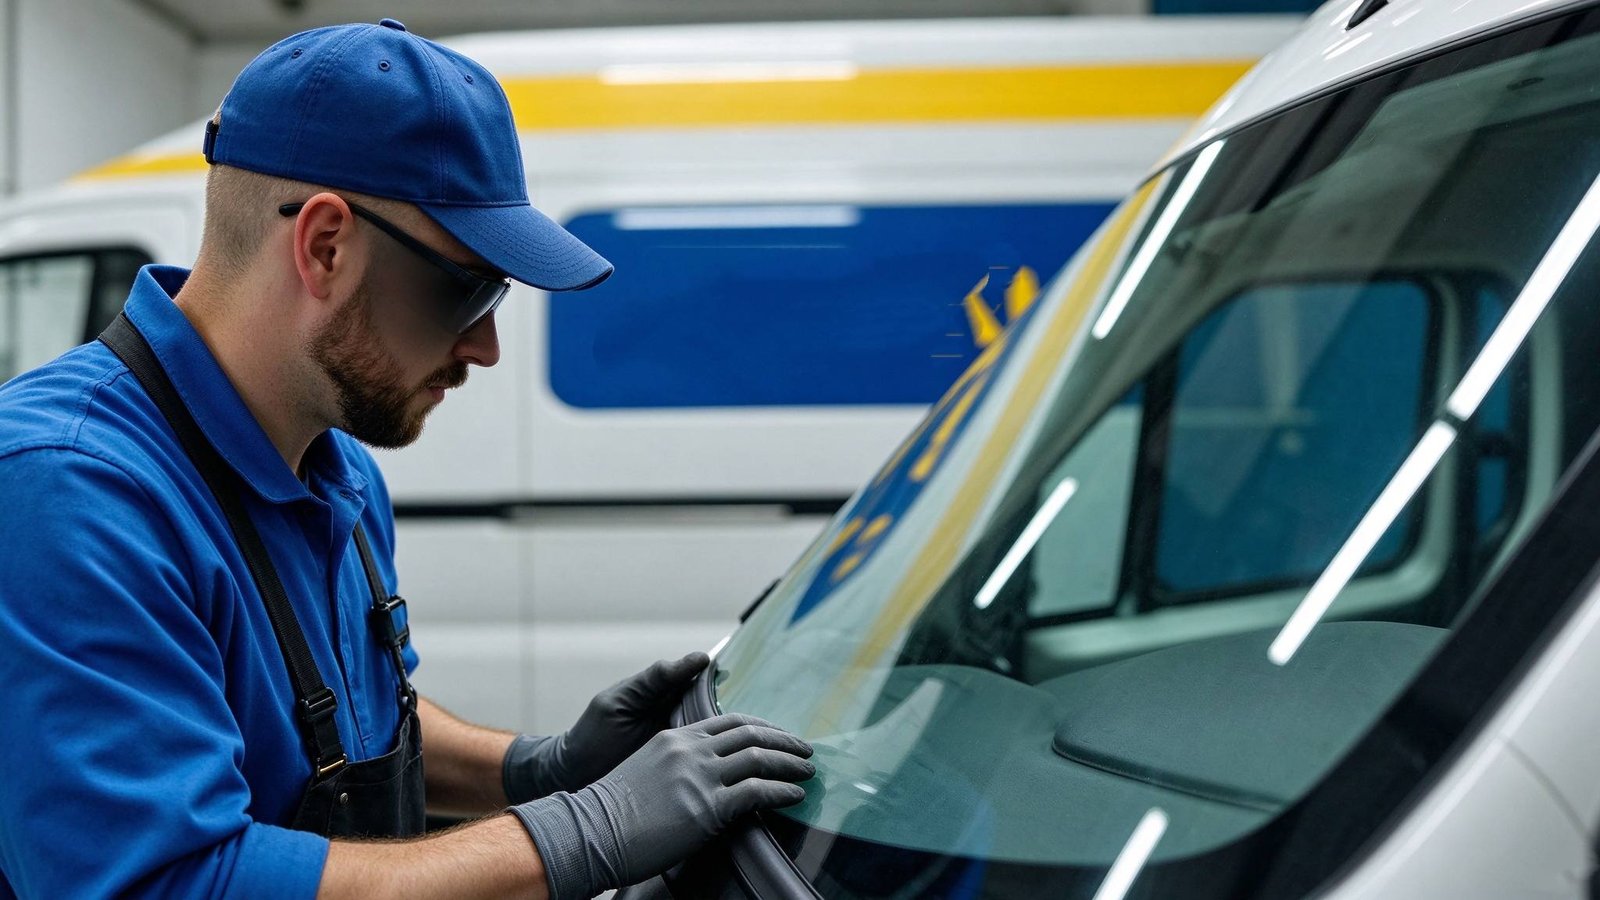
Field auto glass repair facilities encounter severe rust challenges across commercial work vans and aged passenger vehicles.
Scenario A: Express Fleet Van Cowl Rust Restoration
A delivery fleet transit van developed extensive water leakage dripping into the dashboard fuse box. Upon windshield extraction, technicians discovered a 30 cm strip of blistering surface rust along the lower pinchweld cowl.
The shop implemented a full pinchweld rust treatment protocol. Technicians ground the oxidation down to bare metal using an angle grinder with an 80-grit disc, cleaned the area with solvent, and applied a dedicated two-part epoxy pinchweld barrier primer. The vehicle was re-glazed without recurring leaks.
Scenario B: Eliminating Silicone Oil Contamination on Used Vehicles
A pre-owned vehicle received an improper windshield repair where a previous owner pumped clear household silicone into the upper moulding channel to stop a wind whistle.
The technicians removed the silicone mechanically, but invisible siloxane oils remained saturated in paint micro-pores. To achieve compliant windshield pinchweld preparation, technicians executed a rigorous three-pass solvent scrub using specialized wax and grease remover, preventing catastrophic fish-eye dewetting of the fresh polyurethane bead.
Standard Operating Procedure: Complete Pinchweld Decontamination SOP
Adhering to this five-stage decontamination protocol guarantees maximum bond longevity and prevents premature corrosion formation.
Step 1: Urethane Trimming (AGRSS Golden Rule)
Trim the residual polyurethane bead down to a smooth, level thickness of 1 mm to 2 mm using a surgical-grade pinchweld trimming knife. Never scrape down to the painted metal flange unless the underlying coating is loose, cracked, or corroded.
Step 2: Two-Cloth Solvent Degreasing
Dampen a clean, lint-free wipe with an approved aliphatic hydrocarbon or isopropanol cleaner. Wipe firmly in a single forward pass. Immediately follow with a dry, clean lint-free towel to lift emulsified grease before the solvent flashes off.
Step 3: Mechanical Rust Grinding
If rust or bare metal is present, abrade the affected zone down to bare silver steel using an 80-grit abrasive disc. Vacuum away all metal filings using an industrial HEPA vacuum; never use compressed shop air, which blows airborne compressor lubricating oil onto the pinchweld.
Step 4: Chemical Passivation and Primer Coating
Apply an approved anti-corrosion pinchweld barrier primer over bare steel sections using a single-use wool dauber. Allow 15 minutes of flash-off time until the primer achieves a completely matte, tack-free appearance.
Engineer’s Technical Trade-Offs: Remediation Boundaries of Auto Glass Cleaners
Technicians must understand the physical and chemical limits of auto glass chemical cleaners and primers before performing repairs.
- Chemical Primer Thickness Limits: Anti-corrosion primers protect scratches, but applying coatings thicker than 25 microns creates a brittle dry layer prone to micro-cracking under vehicle chassis torsion.
- Severely Perforated Metal: Chemical rust converters and primers cannot restore compromised structural strength on holed pinchweld flanges; perforated metal demands professional body shop panel replacement.
- Solvent Residue Hazards: Utilizing low-grade mineral spirits or oily paint thinners leaves hydrocarbon films that inhibit polyurethane cross-linking, causing total adhesive release.
Frequently Asked Questions: Pinchweld Preparation and Rust Treatment
Why is it recommended to leave 1mm of old urethane on the pinchweld instead of scraping to bare metal?
Existing factory polyurethane provides an ideal, highly compatible bonding substrate for fresh urethane. Scraping down to bare metal damages the OEM cathodic e-coat, increases corrosion risk, and creates fresh scratch channels where moisture can initiate rust delamination.
Can brake cleaner or lacquer thinner be used to degrease a windshield pinchweld?
Technicians should never use brake cleaner or lacquer thinner on window frames. Brake cleaners leave oily hydrocarbon films, while lacquer thinners attack vehicle body paints. Installers must use approved isopropanol or certified wax and grease cleaners.
How soon after applying pinchweld anti-corrosion primer can polyurethane adhesive be extruded?
Technicians must allow a full 10 to 15 minutes of flash-off time at standard room temperature (23°C) until the primer turns completely matte. Extruding urethane over wet primer traps volatile solvents, causing micro-foaming and joint delamination.
Engineering Summary: Flawless Preparation for Lasting Structural Safety
Structural direct glazing is only as durable as the pinchweld substrate beneath it. By preserving intact urethane cushions, aggressively abrading surface rust, and applying specialized anti-corrosive primers, repair centers guarantee flawless bonding and absolute occupant safety across vehicle lifespans.
Authored by ChemPU Automotive Application Engineering Team
Specializing in OEM direct-glazing polyurethane formulation, crash-retention validation per FMVSS 212 standards, and high-performance structural elastomeric bonding solutions for global automotive manufacturers.
Quality Certification: ISO 9001 / IATF 16949 Certified Adhesive Manufacturing
Source Certified OEM Pinchweld Primers & Polyurethane Adhesives
Partner with ChemPU, an ISO 9001 and IATF 16949 certified Chinese manufacturer. We provide anti-corrosion pinchweld primers, specialized surface degreasers, and high-modulus direct glazing polyurethane adhesives for international auto glass distributors and fleet repair networks.
Direct WhatsApp Technical Inquiry: +86 15216655520